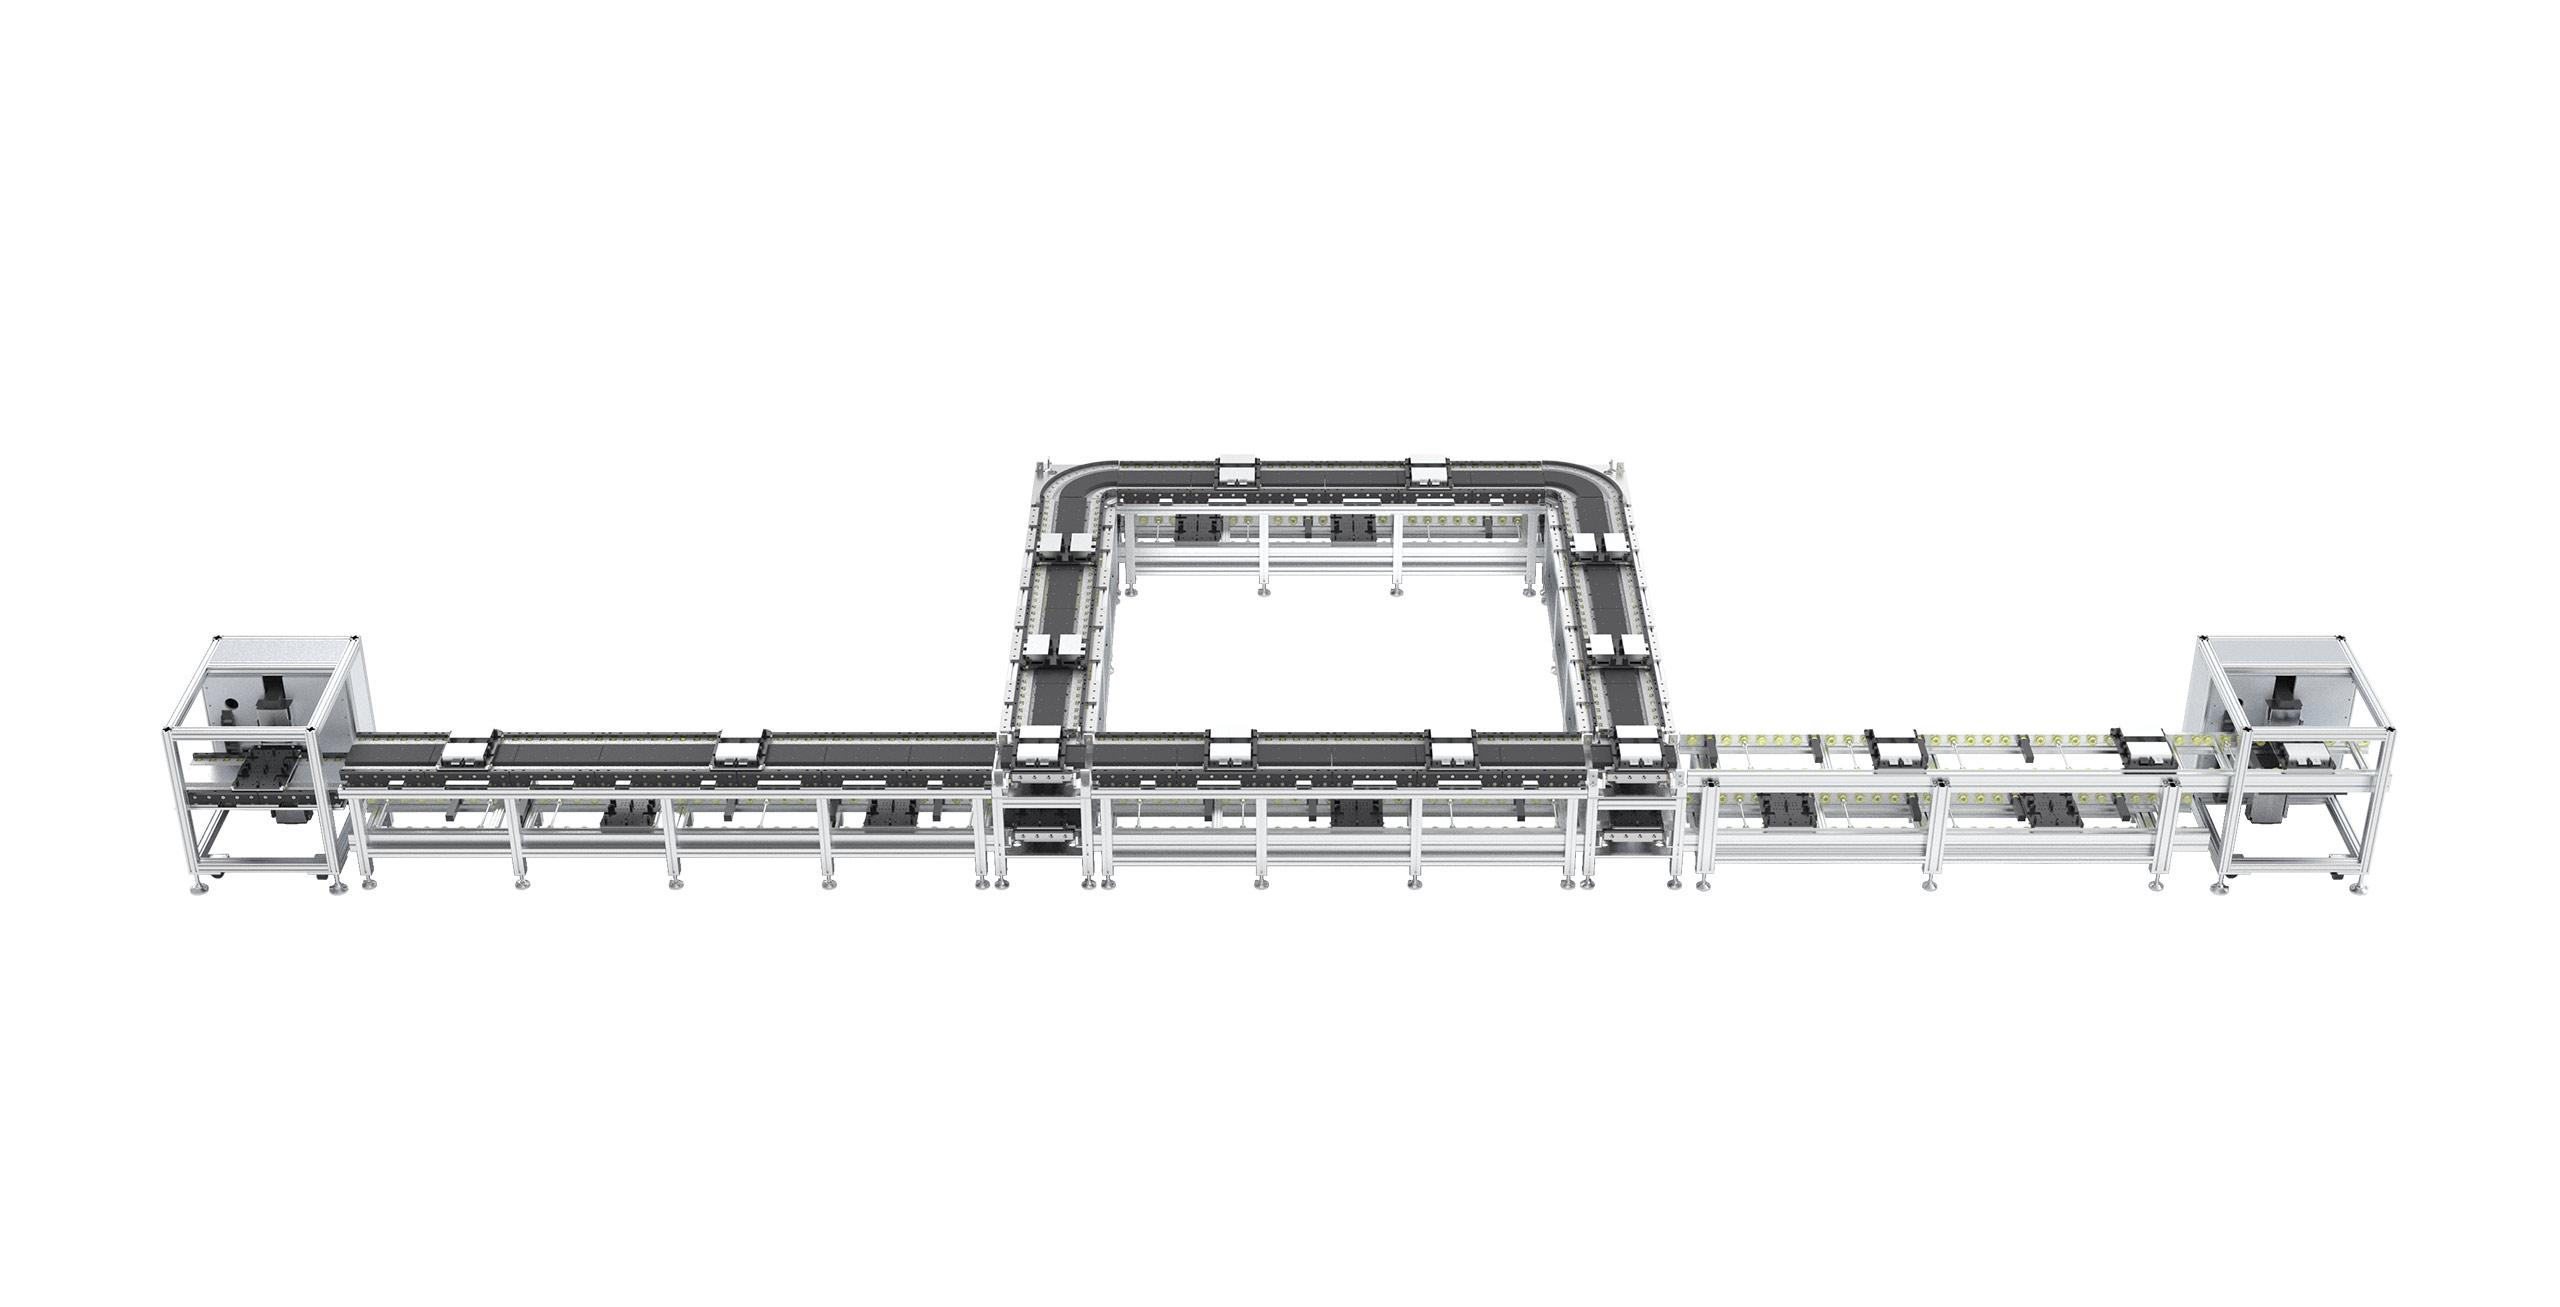
Material movement is a central part of automated manufacturing. Products may pass through assembly, inspection, testing, buffering and packaging before reaching the next production stage. If these transfers are poorly coordinated, individual machines may operate efficiently while the overall line still experiences waiting, accumulation or unnecessary handling.
For this reason, manufacturers are increasingly considering automated pallet conveyor systems as part of a wider material-flow strategy. Their value comes not only from moving products between stations, but also from coordinating movement with production timing and workstation requirements.
Moving Beyond Simple Product Transfer
A conventional conveyor often follows a fixed route. This can work when every product passes through the same sequence. Manufacturing lines, however, may require different products to follow different operations or spend different amounts of time at individual stations.
A flexible pallet transport system can give production engineers more control over these movements. Pallets can be directed to specific workstations, held in designated areas or transferred between sections of the line according to production requirements.
FHS’s FTS-PT logistics transport line is designed for this type of movement. Its product information lists functions including lateral transfer, lifting, rotary transfer, docking and curved transport, allowing the transport architecture to adapt to different production layouts.
Keeping Workstations in Step
Material flow becomes more complicated when processes have different cycle times. If one station finishes earlier than the next, products may need temporary buffering rather than stopping the entire line.
An intelligent transport system can coordinate pallet positions according to workstation status. This creates opportunities to separate individual process cycles while maintaining a connected production flow.
FHS’s flexible transport software architecture supports intelligent scheduling and external workstation synchronisation. Its iFCS control software supports configurable workstation scheduling and individual mover control, while iFTS-Studio is used for system configuration and debugging.
For manufacturers, conveyor planning should therefore be considered alongside machine cycle time. The transport system needs sufficient flexibility to handle normal production variations without creating unnecessary accumulation.
Routing Products According to Process Needs
Not every product needs to follow exactly the same route. Some products may require additional inspection, while others may need to bypass a process or move to another station after a quality check.
Flexible routing can address this requirement. Instead of building multiple independent conveyor lines, manufacturers can design a transport network capable of directing products according to defined production conditions.
The FTS-PT system supports modular configuration and can be combined with conventional conveyor equipment. Its published specifications include a typical load of up to 40 kg, a maximum speed of 2.5 m/s and repetitive positioning accuracy of ±0.1 mm. It also supports modular expansion for changing production layouts.
The appropriate configuration still depends on payload, product dimensions, takt time and workstation arrangement.
Using Pallets to Support Production Traceability
A pallet can support production traceability when its identity is linked with the product and relevant manufacturing data. This can help production teams identify where a product entered the line, which stations it passed through and whether additional inspection is required. Such traceability can be useful when different products share the same equipment.
The broader flexible transport technology of FHS supports real-time mover identification and defect-based scheduling. When a defective product is detected, the system can direct it towards a designated unloading station instead of continuing through the standard route.
Connecting Transport With Automation Equipment
A conveyor should not be planned as an isolated piece of equipment. Its controls need to communicate with robots, inspection systems, assembly machines and factory-level software.
FTS-PT supports industrial communication interfaces including EtherCAT, Modbus/TCP, PROFINET, CC-Link, CANopen and POWERLINK. This gives engineers options when integrating the transport system into an existing automation architecture.
The control layer is equally important. FHS’s software tools support graphical track configuration, workstation setup, system monitoring, simulation and parallel debugging. These functions can help engineers evaluate movement logic during project implementation.
Preparing the Line for Change
Production requirements can change after an automation line has been installed. New products may require different tooling, additional inspection or revised routing. A transport system that is difficult to modify can make these changes more complicated.
Manufacturers can therefore assess whether additional movers, workstations or transport sections can be incorporated as requirements develop. Modular equipment can provide a more practical approach when future changes are expected.
Improving the Complete Material Flow
The purpose of pallet conveyors automation systems is not simply to move products between machines. Their role is to connect production stages, manage different cycle times, support routing decisions and provide controlled movement across the manufacturing process.
FHS provides flexible transport technologies that can be evaluated according to payload, speed, positioning requirements and workstation configuration. Its FTS-PT platform shows how transport and control can be combined within an automated production environment.
For manufacturers planning a new line or upgrading an existing one, the starting point should be the complete material-flow map. Once movement requirements and process connections are understood, the conveyor architecture can be selected to support the production system as a whole.
